How to Choose the Right Contract Manufacturer for Snack Brand
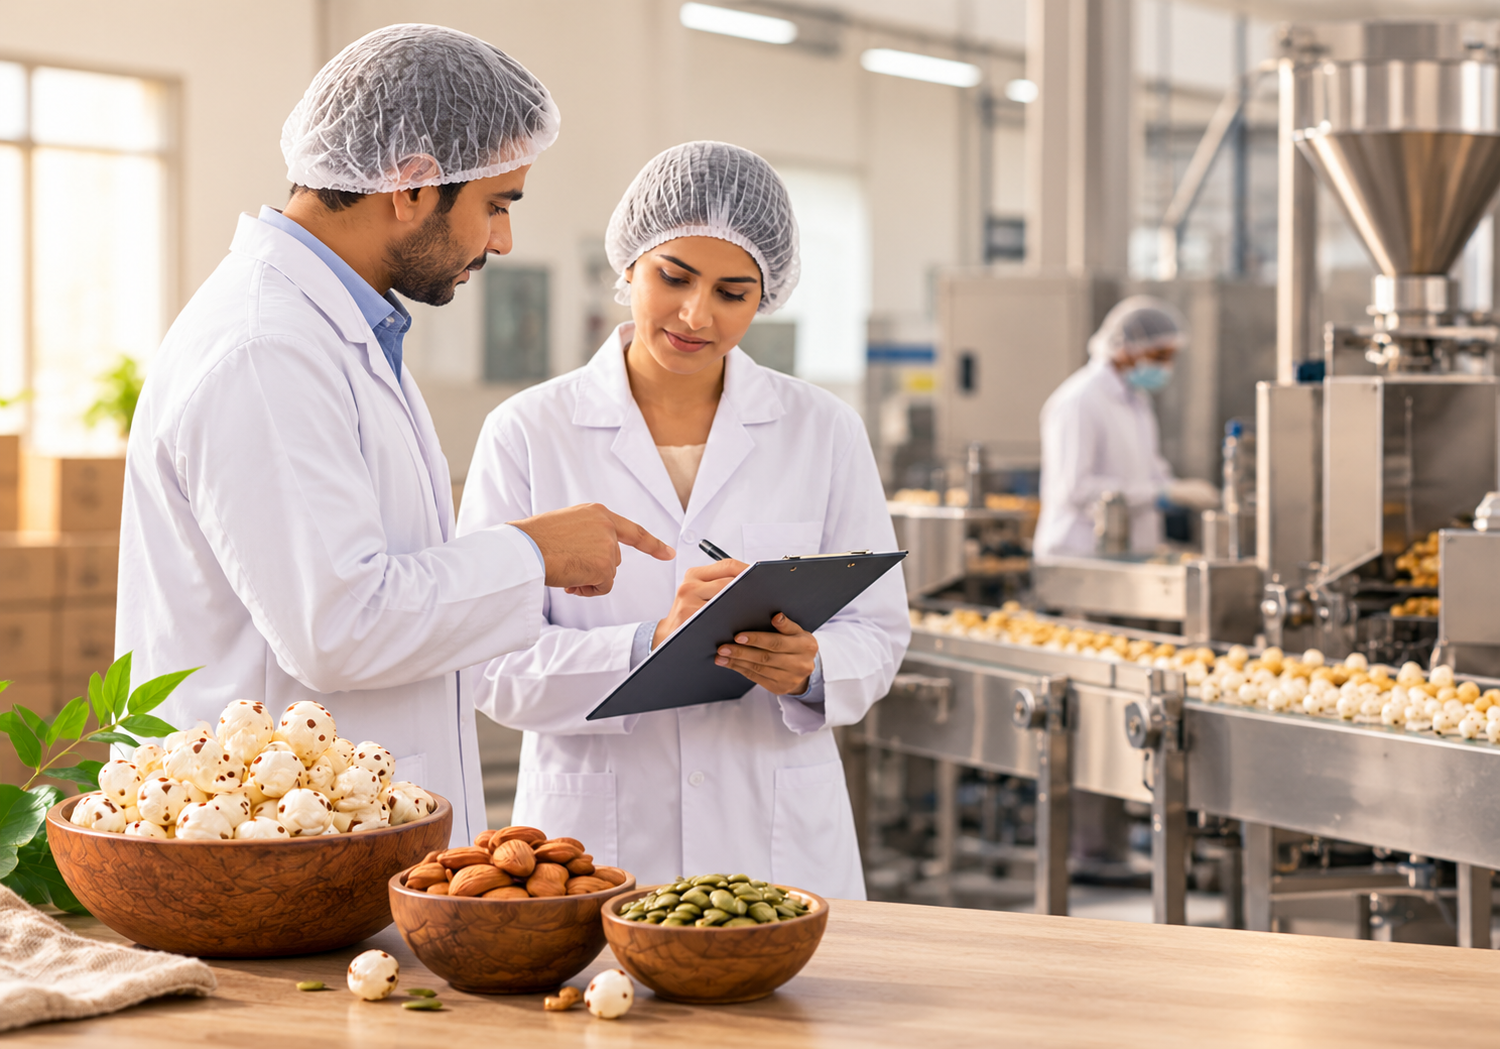
Choosing a contract manufacturer is one of the most consequential decisions a snack brand makes. Get it right and you have a supply chain that supports your growth, your quality standards and your brand story. Get it wrong and you are dealing with inconsistent product, missed timelines and customer complaints that take years to recover from.
Most first-time brand founders spend more time on packaging design and flavour names than they do on evaluating their manufacturer. That is understandable. The visible parts of a brand are easier to think about than a factory visit checklist. But this article is meant to correct that balance. Here is what to look for, what to ask and what the answers tell you about a contract manufacturer for your snack brand.
![]()
Why the Manufacturer Choice Matters More Than You Think
The manufacturer is not just the factory where your product is made. They are the entity responsible for every ingredient that goes into your product, the process by which it is made, the hygiene conditions under which it is packed and the consistency of what your customers receive across every batch. A good product concept with a weak manufacturing partner produces an inconsistent product. An inconsistent product produces customer complaints, returns and negative reviews. In a category like healthy snacks, where repeat purchase drives profitability, inconsistency is a brand problem that compounds over time. The right contract manufacturer does not just make your product. They become an operational foundation your brand builds on. The time you invest in choosing well at the start saves you significantly more time managing problems later.Step 1: Verify Certifications Before Anything Else
Any contract manufacturer operating in the Indian food industry must hold a valid FSSAI licence. This is the baseline. Without it, the facility cannot legally produce packaged food products for commercial sale. Beyond FSSAI, look for ISO certifications. ISO 9001:2015 covers quality management systems, which means the facility has documented processes for how they operate and a system for tracking and addressing quality issues. ISO 22000:2018 is a food safety management standard that specifically addresses risks in the food production chain from raw material to finished product. A contract manufacturer who holds FSSAI, ISO 9001:2015 and ISO 22000:2018 has been through external audits and demonstrated that their processes meet an independent standard. That is significantly more meaningful than a self-described commitment to quality. Ask to see the certificates. Check the expiry dates. A lapsed certificate is a red flag, and a manufacturer who cannot produce them at all should not be producing food at commercial scale.Step 2: Understand Their Product Range and Specialisation
Not every contract manufacturer is right for every product. A facility that specialises in fried namkeen is not the right partner for a brand building on roasted, clean-label snacks. A manufacturer whose primary output is biscuits may not have the equipment, calibration or process knowledge for Makhana. Ask specifically what product categories the facility has experience with. Ask to see samples from existing production runs, not custom samples made to impress you during a sales conversation. Existing production samples show you what the factory regularly produces, not what it can produce when trying to win your business. A contract manufacturer with deep experience in your specific category will have better raw material sourcing relationships, better process calibration and clearer quality benchmarks than a generalist facility that makes a little of everything.Step 3: Ask About Raw Material Sourcing
Where ingredients come from affects the finished product. This is true for every category but especially in health snacks, where raw material quality directly affects the nutritional profile, texture and clean-label positioning of what reaches the shelf. Ask your manufacturer specifically where they source their primary raw materials. For Makhana, ask whether the raw Makhana comes from Bihar, which is the established quality benchmark for this ingredient in India. For roasted nuts, ask about the source and grade. For Khakhra and Bhakhri, ask about flour sourcing and milling standards. A contract manufacturer who can answer these questions specifically is one who is engaged with their supply chain. One who cannot answer them is one buying from the cheapest available price point, which typically means inconsistent raw material quality across batches and inconsistent finished product across packs.Step 4: Evaluate Manufacturing Process Transparency
Ask the manufacturer to explain exactly how they make the product. Not in general terms, but specifically. What equipment do they use? What temperature does the roasting process run at? How long does a batch take? How do they check quality mid-process? The answers matter less than the fact that they can give them at all. A contract manufacturer who knows their own process in detail is one who is in control of it. One who gives vague answers, redirects to finished product samples or cannot explain why their process produces the result it does is one where quality control is informal at best. Specific process details are also the foundation of your brand story. If your manufacturer uses a double flame roasting process that produces more even heat distribution than a single heat source, that is something you can say clearly in your marketing. If the process is vague and undocumented, there is nothing specific to communicate to your customer.Step 5: Check Production Capacity and Scalability
You need a contract manufacturer who can handle your current volume. You also need one who can grow with you without the growth affecting quality or timelines. Ask about annual production capacity. Ask how many other brands or clients the facility currently produces for and what percentage of that capacity they are currently running at. Ask what the typical lead time looks like at different order volumes. Ask about minimum and maximum order quantities in your product category. A manufacturer running at full utilisation has no room to absorb your growth without something giving. A manufacturer with unused capacity can scale with your brand as demand increases. The capacity question also tells you something about how organised the facility is, since a well-run contract manufacturer tracks this kind of data precisely rather than estimating.Step 6: Assess Private Label and Packaging Capability
A contract manufacturer set up for private label and white label business has different capabilities from one that primarily does bulk commodity supply. For a branded product, you need a manufacturer who can work with your packaging specifications, your design files and your labelling requirements throughout the production process. Ask whether packaging is handled in-house. Ask whether the facility can accommodate different pouch formats, zip-lock, stand-up pouches, jars or custom pack dimensions. Ask what the process looks like for approving packaging and artwork before a production run starts. Ask what the minimum run is for a new SKU or pack size. A contract manufacturer who is properly set up for private label clients will have clear, documented answers to all of these questions. They will have handled the onboarding process for multiple brands before you and will know exactly how to bring your packaging into production.Red Flags to Watch For
Unwillingness to show the facility is a significant concern. Any reputable contract manufacturer should be willing to have potential clients visit the production floor, storage areas and packing section. A facility that resists or creates obstacles to a visit raises an obvious question about what it is avoiding. Vague answers about certifications, processes or sourcing are a consistent warning sign. Reputable manufacturers are proud of what they have built. They want to show you their certifications and explain their process. Evasiveness in any of these areas suggests something is being managed rather than shared. Pricing well below market rate almost always means cost has been cut somewhere in raw material quality, hygiene standards, process consistency or labour. In food manufacturing, those cuts show up in the product. A brand that competes on quality cannot afford a manufacturing partner that competes on the lowest price. No references from existing clients is a concern for any established facility. A contract manufacturer who has produced for other brands should be able to point you to businesses they have worked with. If they cannot or will not, ask why.How to Think About the Decision
Treat manufacturer selection as a due-diligence process, not a purchasing decision. You are not buying production capacity. You are choosing an operational partner whose decisions affect every pack of product that reaches your customer. The cheapest option rarely reflects the true cost once you factor in inconsistent quality, rejected batches, customer returns, stock write-offs and the time spent managing a supplier who is not set up to support a growing brand. The right contract manufacturer for your snack brand makes your product consistently, speaks clearly about how and why they do what they do, and has the certifications, capacity and process maturity to support a brand building for the long term.How Purva Bites Fits This Criteria
Purva Bites is a contract manufacturer based in Udaipur, Rajasthan, holding FSSAI, ISO 9001:2015 and ISO 22000:2018 certifications. Annual production capacity is 1,000 MT across Makhana, Khakhra, Bhakhri, roasted seeds, roasted nuts and extrusion-based products. All raw Makhana is sourced from Bihar. Roasting uses a double flame process with no palm oil added at any stage. Packaging is handled in-house with support for custom pack sizes, private label specifications and multiple SKUs across all product categories. Dispatch is available pan-India. If you are evaluating a contract manufacturer for your snack brand and want to understand whether Purva Bites is the right fit for your requirement, get in touch with our team. Contact us to discuss your manufacturing requirementFrequently Asked Questions
What certifications should a snack contract manufacturer have in India? The minimum is a valid FSSAI licence. ISO 9001:2015 for quality management and ISO 22000:2018 for food safety are the additional certifications that show a facility with documented, externally audited processes. Ask to see the certificates and check the expiry dates. What questions should I ask a contract manufacturer before signing? Ask about certifications and when they were last audited. Ask where they source their primary raw materials. Ask them to explain their manufacturing process in detail. Ask about annual production capacity, current utilisation, minimum order quantities and lead times. Ask for samples from existing production runs rather than samples made specifically for your visit. How do I know if a contract manufacturer is set up for private label? A manufacturer set up for private label will have clear processes for working with your packaging specifications, design files and label requirements. They will handle packaging in-house, support multiple SKUs and have an established process for onboarding new private label clients. If they cannot explain this process clearly, they are likely not set up for it. What is the difference between contract manufacturing and white label? In contract manufacturing, the product is made to your specific formulation and requirements. In white label, the manufacturer has existing formulations that you choose from and brand as your own. Contract manufacturing gives you more control and product differentiation. White label gets you to market faster with less development investment. Can a contract manufacturer scale with my brand as volumes grow? It depends on the facility's total capacity and how fully utilised it currently is. Ask specifically about annual production capacity and current utilisation before committing. A manufacturer running at full capacity cannot absorb your growth without it creating pressure on timelines or affecting quality for other clients.Related Articles
Bihar Makhana vs Other Makhana - Why Sourcing Matters for Your Brand
If you are building a private label Makhana brand, one of the first questions worth asking your manufacturer is where their raw Makhana comes…
What Is Single vs Double Flame Roasting? A Simple Explanation
Most snack brands say their products are roasted. Very few explain how. When you look at the manufacturing process, the method used to apply…
Why Makhana Is the Fastest Growing Snack Category for Private Label Brands
A few years ago, Makhana was mostly a fasting food. You found it in homes during Navratri, in temple offerings, and occasionally in a…